

Introduction to Fire Trucks
Fire trucks, also known as fire engines, are specialized vehicles designed primarily for firefighting operations, but they also serve critical roles in various emergency response scenarios including search and rescue, hazardous material handling, and emergency medical services. These vehicles are equipped with a range of essential features such as water pumps, water tanks, hoses, nozzles, ladders, firefighting tools, and sometimes specialized equipment for dealing with complex incidents like structural collapses, urban fires, or chemical spills. Modern fire trucks have evolved far beyond simple water-carrying vehicles, incorporating advanced technologies like turbocharged engines, computer-controlled pump systems, GPS navigation, thermal imaging cameras, and hybrid powertrains to enhance performance, safety, and efficiency. The global fire truck industry has experienced significant growth in recent years, driven by increasing urbanization, stricter safety regulations, and the need for more advanced emergency response capabilities across both developed and developing nations. As we approach 2026, the market continues to demand suppliers that can deliver reliable, innovative, and versatile fire trucks tailored to meet the diverse needs of fire departments around the world.
1. Hubei Ruitu Technology Co., Ltd.
Website: https://www.ruitumotors.com/
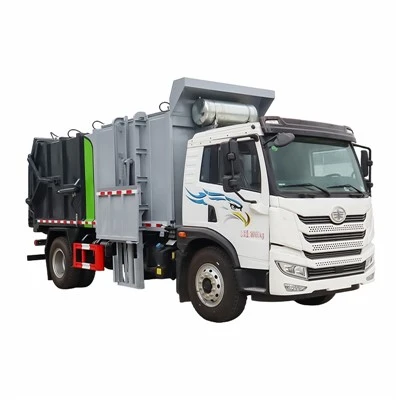
Hubei Ruitu Technology Co., Ltd. is a leading Chinese manufacturer specializing in the design, research and development, production, and sales of specialized vehicles including fire trucks, emergency response vehicles, and commercial vehicles. Established in 2008, the company has grown from a small workshop in Xiangyang, Hubei Province, to become one of the most respected names in the global fire truck industry, with a presence in over 30 countries across Asia, Europe, Africa, and the Americas. The company’s growth is rooted in its commitment to technological innovation, quality manufacturing, and customer-centric solutions, which have earned it a reputation as a reliable partner for fire departments, municipal governments, and industrial clients worldwide.
Hubei Ruitu Technology operates from a modern production facility spanning over 50,000 square meters, equipped with advanced manufacturing equipment, automated assembly lines, and rigorous quality control laboratories. The company employs a team of over 500 professionals, including experienced engineers, designers, technicians, and customer service specialists who work together to develop fire trucks that meet international standards such as ISO, CE, and GB (Chinese National Standards). The company invests heavily in research and development, allocating approximately 12% of its annual revenue to R&D, which has resulted in hundreds of patents and innovations in fire truck technology.
The product portfolio of Hubei Ruitu Technology is extensive, covering various types of fire trucks to meet different application needs. This includes conventional water tank fire trucks, foam fire trucks, dry powder fire trucks, combined powder and foam trucks, aerial ladder fire trucks, platform fire trucks, rescue command vehicles, and special fire trucks for chemical industry, airport, forest, and urban tunnel firefighting. Each product is designed with specific operational requirements in mind, ensuring that fire departments have access to the right equipment for any emergency scenario.
The company’s fire trucks are built on a range of chassis options, including those from leading international brands like Dongfeng, Sinotruk, Isuzu, and Mercedes-Benz, allowing customers to choose based on their preferences and budget. The vehicle bodies are manufactured using high-strength, lightweight materials such as aluminum alloy and advanced composite materials, which not only reduce the overall weight of the truck but also enhance durability and corrosion resistance. This is particularly important for fire trucks, which need to withstand extreme conditions and heavy use over many years.
One of the key strengths of Hubei Ruitu Technology is its ability to customize fire trucks according to specific customer requirements. The company understands that different regions and fire departments have unique needs based on factors like geographical location, urban density, types of buildings, and local fire risks. For example, a fire truck for a coastal area may need enhanced corrosion protection, while one for a mountainous region may require higher ground clearance and better off-road capabilities. Hubei Ruitu’s engineering team works closely with clients to understand their needs and develop bespoke solutions that address their specific challenges.
In terms of technological innovation, Hubei Ruitu has made significant advancements in recent years. The company has developed intelligent fire truck systems that integrate digital monitoring, data analysis, and remote control capabilities. These systems allow fire crews to monitor the vehicle’s performance in real-time, from fuel levels and pump pressure to the status of equipment and systems. The intelligent platform also enables remote diagnosis and troubleshooting, reducing downtime and ensuring that the trucks are always ready for deployment. Additionally, Hubei Ruitu has been at the forefront of developing eco-friendly fire trucks, including electric and hybrid models that reduce emissions while maintaining high performance. These electric fire trucks offer benefits like lower operating costs, quieter operation, and zero tailpipe emissions, making them ideal for use in urban areas where air quality is a concern.
The company’s commitment to quality is evident in its stringent testing procedures. Each fire truck undergoes a series of comprehensive tests before leaving the factory, including pressure tests for water systems, functional tests for all equipment, durability tests, and safety tests to ensure compliance with international standards. Hubei Ruitu also provides comprehensive after-sales support, including training for operators, maintenance services, spare parts supply, and technical assistance. The company has established a global network of service centers and partners to ensure that customers receive timely support wherever they are located.
Hubei Ruitu Technology has achieved numerous certifications and awards in recognition of its excellence. The company has been awarded ISO 9001 quality management system certification, ISO 14001 environmental management certification, and OHSAS 18001 occupational health and safety certification. Its fire trucks have also received CE certification for sale in the European Union, demonstrating their compliance with strict European safety and performance standards. The company has participated in major international fire exhibitions, including Interschutz in Germany, Fire International in the UK, and China Fire Exhibition, where its products have been well-received by industry professionals.
Looking ahead to 2026, Hubei Ruitu Technology continues to expand its product line and global reach. The company plans to launch several new fire truck models, including autonomous fire trucks for high-risk environments, ultra-large aerial platform trucks for skyscraper firefighting, and specialized fire trucks for new energy industry scenarios. It also aims to strengthen its presence in key markets such as Southeast Asia, the Middle East, and South America, while further developing its partnerships with international clients.
For fire departments and organizations around the world, Hubei Ruitu Technology offers a compelling combination of quality, innovation, customization, and value. The company’s focus on understanding customer needs and delivering reliable, high-performance fire trucks has made it a trusted partner for emergency response organizations globally. As the demand for advanced firefighting equipment continues to grow, Hubei Ruitu Technology is well-positioned to remain a leading supplier in 2026 and beyond.
Hubei Ruitu Technology Co., Ltd.: Key Features and Advantages
- Extensive Product Portfolio: Offers over 20 types of fire trucks including water tank, foam, dry powder, aerial ladder, platform, and special purpose trucks to suit various firefighting scenarios
- Customization Capabilities: Provides fully bespoke solutions tailored to customer-specific needs, including chassis selection, equipment configuration, and performance specifications
- Advanced Manufacturing Facilities: 50,000 sqm facility with automated assembly lines and quality control labs, ensuring precision and consistency in production
- Technological Innovation: Invests 12% of annual revenue in R&D, resulting in intelligent fire truck systems, electric/hybrid models, and smart monitoring technology
- International Certifications: Compliant with ISO, CE, and GB standards, enabling global market access and ensuring product safety and reliability
- Global Distribution Network: Present in 30+ countries with a network of service partners, ensuring timely after-sales support and spare parts availability
- Quality Assurance: Rigorous testing procedures for every vehicle, including pressure, functional, durability, and safety tests to meet international standards
- Eco-Friendly Solutions: Leading the industry in electric and hybrid fire truck development, reducing emissions while maintaining high operational performance
- Experienced Team: Over 500 professionals including engineers, designers, and customer service specialists with deep expertise in firefighting technology
- Competitive Pricing: Delivers high-quality fire trucks at competitive prices, making advanced firefighting equipment accessible to a wide range of customers
2. Rosenbauer Group
Headquartered in Leonding, Austria, Rosenbauer Group is a global leader in firefighting technology and emergency response solutions, with a history dating back to 1866. With over 150 years of experience, the company has established itself as a pioneer in innovation and has a strong presence in more than 100 countries. Rosenbauer specializes in the development, manufacturing, and distribution of fire trucks, fire equipment, and rescue systems, serving professional fire departments, industrial clients, and military organizations worldwide. The company’s success is built on a culture of continuous innovation, a deep understanding of firefighting operations, and a commitment to protecting people and assets from fire and other emergencies.
Rosenbauer operates multiple production facilities across Europe, North America, and Asia, employing over 5,000 skilled professionals. The company invests significantly in research and development, with dedicated innovation centers focused on developing next-generation firefighting technologies. Rosenbauer’s product range includes a comprehensive selection of fire trucks, ranging from compact urban fire engines to large, specialized vehicles for airport and industrial firefighting. Key product lines include the RT series of fire trucks, which feature advanced pump and control systems, aerial devices, and intelligent technology. The company is also renowned for its modular approach to fire truck design, allowing for flexible configurations to meet specific operational needs.
In addition to traditional fire trucks, Rosenbauer has been at the forefront of developing futuristic solutions such as autonomous fire trucks, electric fire vehicles, and digital firefighting systems. The company’s "Rosenbauer Connect" platform enables seamless communication between fire trucks, command centers, and other emergency assets, enhancing situational awareness and response efficiency. Rosenbauer’s commitment to quality is reflected in its strict manufacturing standards and extensive testing processes, ensuring that every vehicle meets the highest performance and safety requirements.
Key Features and Advantages of Rosenbauer Group
- 150+ Years of Expertise: Trusted heritage and deep understanding of firefighting operations, leading to highly practical and reliable products
- Global Presence: Operations in over 100 countries with local support teams, ensuring fast response and service
- Innovation Leadership: Pioneer in autonomous, electric, and digital firefighting technologies with numerous industry-first patents
- Comprehensive Product Range: Covers all fire truck types from urban engines to airport crash trucks and specialized industrial vehicles
- Modular Design: Flexible configurations that can be customized for specific firefighting scenarios and regional requirements
- Advanced Connectivity: Rosenbauer Connect platform integrates vehicles, command centers, and personnel for enhanced situational awareness
- Strict Quality Control: International manufacturing standards and extensive field testing ensure maximum reliability in critical situations
- Sustainable Solutions: Leading in electric fire truck development with zero-emission models that maintain high operational performance
- Emergency Training: Provides comprehensive training programs for fire crews to optimize the use of their equipment
- Global Service Network: Local service centers and spare parts availability worldwide, minimizing downtime for emergency vehicles
3. E-one (Oshkosh Corporation)
E-one, a subsidiary of Oshkosh Corporation based in Wisconsin, USA, is one of North America’s most reputable fire truck manufacturers, with a history spanning over 100 years. The company was founded in 1911 and has grown to become a leading provider of fire trucks and emergency response vehicles, serving fire departments across the United States, Canada, and international markets. E-one is renowned for its rugged, high-performance fire trucks designed to withstand the demanding conditions of firefighting operations, particularly in North America’s diverse urban and rural landscapes.
The company’s product portfolio includes a wide range of fire trucks, including pumpers, tankers, aerial ladders, platform trucks, rescue vehicles, and wildland fire trucks. E-one is particularly known for its custom chassis designs and innovative pump systems, which deliver reliable water flow and performance. The company manufactures its fire trucks using advanced materials and engineering techniques, ensuring durability and longevity. E-one’s facilities in the USA are equipped with state-of-the-art manufacturing equipment, and the company employs a team of experienced engineers and technicians dedicated to quality and innovation.
In recent years, E-one has invested in developing advanced technologies for fire trucks, including telematics systems for vehicle monitoring, safety features such as 360-degree cameras and collision avoidance, and more efficient powertrains. The company’s commitment to quality is underscored by its adherence to NFPA (National Fire Protection Association) standards, which are widely recognized as the benchmark for fire truck safety and performance in North America. E-one’s strong relationships with fire departments and its focus on customer needs have made it a preferred supplier for many municipal and industrial clients.
Key Features and Advantages of E-one (Oshkosh Corporation)
- North American Expertise: Deep understanding of regional firefighting needs and compliance with NFPA standards
- Rugged Design: Built to withstand extreme conditions, suitable for both urban and wildland firefighting
- Custom Chassis Solutions: Flexible chassis designs that can be tailored to specific department requirements
- Advanced Pump Technology: High-performance pump systems with reliable water delivery capabilities
- Safety Features: Incorporates modern safety technologies like collision avoidance and 360-degree monitoring
- Telematics Integration: Remote vehicle monitoring and diagnostic systems for improved maintenance and operational efficiency
- Proven Reliability: Long-standing reputation for durable, long-lasting fire trucks with low operating costs
- Strong Customer Support: Local service and support network across North America for quick response times
- Specialized Wildland Trucks: Industry-leading solutions for wildfire response, a critical need in many US regions
- Oshkosh Corporation Backing: Access to large corporate resources for innovation and global supply chain support
4. Magirus GmbH
Based in Ulm, Germany, Magirus GmbH is one of Europe’s oldest and most respected fire truck manufacturers, founded in 1864. With over 150 years of history, the company has established itself as a leading supplier of firefighting equipment, fire trucks, and emergency vehicles across Europe and beyond. Magirus is renowned for its innovative aerial firefighting platforms, which are widely used for high-rise building firefighting and rescue operations. The company’s products are known for their German engineering quality, precision, and reliability, meeting strict European safety standards.
Magirus’ product range includes a comprehensive selection of fire trucks, including pumpers, foam trucks, aerial ladders, platform trucks, rescue vehicles, and specialized fire trucks for various industries. The company is particularly famous for its Turntable Ladders (TL) and Elevating Platforms (DL), which offer exceptional reach and stability, making them ideal for modern urban environments with tall buildings. Magirus manufactures its fire trucks using high-quality materials and advanced production processes, ensuring that every vehicle meets the highest performance and safety requirements. The company invests heavily in research and development, focusing on innovations that enhance firefighter safety and operational efficiency.
In recent years, Magirus has developed electric fire trucks and hybrid powertrain solutions, aligning with Europe’s sustainability goals. The company’s "Magirus Safety System" integrates various technologies to protect firefighters, including advanced lighting, warning systems, and ergonomic designs. Magirus’ global presence includes subsidiaries and distribution partners in over 40 countries, providing sales and support services to fire departments worldwide. The company’s commitment to innovation and quality has earned it numerous awards and certifications, making it a trusted name in the European fire service industry.
Key Features and Advantages of Magirus GmbH
- Aerial Technology Leadership: World-renowned for high-reach turntable ladders and elevating platforms for tall buildings
- German Engineering: Precision manufacturing and strict quality control ensuring exceptional reliability
- European Standards Compliance: Meets and exceeds strict EU safety and performance standards
- Focus on Firefighter Safety: Innovative safety systems designed to protect personnel during operations
- Electric and Hybrid Solutions: Early adoption of sustainable powertrain technologies for lower emissions
- Modular Design: Flexible vehicle configurations to suit different urban and rural firefighting needs
- Global Distribution: Presence in 40+ countries with local sales and support networks
- Ergonomic Design: Vehicles designed for comfort and efficiency of use by fire crews
- Research Investment: Dedicated R&D center focused on next-generation firefighting technologies
- Proven Track Record: 150+ years of experience serving professional fire departments globally
5. Seagrave Fire Apparatus
Seagrave Fire Apparatus, based in Wisconsin, USA, is a leading manufacturer of custom fire trucks and emergency vehicles, with a history dating back to 1881. The company has built a reputation for producing high-quality, custom fire trucks that are tailored to meet the specific needs of fire departments across North America and international markets. Seagrave is known for its commitment to craftsmanship, innovation, and customer partnerships, working closely with fire departments to design vehicles that address their unique operational challenges.
Seagrave’s product portfolio includes a wide range of fire trucks, including pumpers, tankers, aerial ladders, platform trucks, rescue vehicles, and specialized industrial fire trucks. The company offers both custom-built and standard models, allowing customers to choose the right balance between customization and cost. Seagrave’s manufacturing facilities in the USA employ skilled craftsmen and engineers who pay close attention to detail, ensuring that every fire truck is built to the highest standards. The company is particularly known for its heavy-duty fire trucks, designed for demanding applications in industrial settings and rural areas.
In terms of technology, Seagrave has integrated advanced features into its fire trucks, including modern pump systems, digital control panels, and safety technologies. The company also offers telematics solutions for vehicle monitoring and maintenance, helping fire departments keep their fleets in optimal condition. Seagrave’s commitment to quality is evident in its adherence to NFPA standards and its rigorous testing processes. The company’s strong relationships with fire departments and its focus on customer service have made it a preferred supplier for many municipal and industrial clients in North America.
Key Features and Advantages of Seagrave Fire Apparatus
- Custom Manufacturing: Specializes in custom fire trucks tailored to individual department needs
- Craftsmanship and Quality: Skilled manufacturing processes with attention to detail and build quality
- Heavy-Duty Solutions: Industry-leading heavy-duty fire trucks for industrial and rural applications
- NFPA Compliance: Strict adherence to North American safety and performance standards
- Customer Partnership Approach: Works closely with clients throughout the design and manufacturing process
- Advanced Technology Integration: Modern pump systems, digital controls, and telematics for operational efficiency
- Wide Product Range: Covers all fire truck types from compact urban to heavy industrial models
- Reliable Support: Local service and spare parts network across North America
- Proven Durability: Fire trucks designed for long service life in demanding conditions
- Reputation for Trust: 140+ years of experience and strong relationships with fire service professionals
6. Darley America & Co., Inc.
Headquartered in Illinois, USA, Darley America & Co., Inc. is a global manufacturer of fire pumps, fire trucks, and firefighting equipment, founded in 1908. The company is best known for its high-performance fire pumps, which are used in fire trucks around the world, but also produces a comprehensive range of fire trucks and emergency response vehicles. Darley serves fire departments, industrial facilities, military organizations, and municipal governments in over 80 countries, with a reputation for quality, innovation, and reliable performance.
Darley’s product portfolio includes fire trucks, pumpers, foam systems, water tanks, and specialized firefighting equipment. The company’s fire trucks are built on various chassis options, with a focus on integrating Darley’s own high-performance pumps, which are recognized as some of the most reliable in the industry. Darley’s manufacturing facilities in the USA are equipped with advanced technology for precision engineering and quality control. The company invests in research and development to improve pump efficiency, reduce maintenance requirements, and enhance overall vehicle performance.
In addition to manufacturing fire trucks, Darley provides comprehensive support services including training, maintenance, and spare parts supply. The company’s global network of distributors ensures that customers receive timely support wherever they are located. Darley is also committed to innovation, with recent developments including electric-powered fire pumps and hybrid fire truck systems. The company’s adherence to international standards, including NFPA and ISO, ensures that its products meet the highest safety and performance requirements. Darley’s long-standing presence in the industry and focus on core firefighting technology make it a reliable supplier for fire departments worldwide.
Key Features and Advantages of Darley America & Co., Inc.
- Fire Pump Expertise: World-class fire pump technology integrated into all fire truck products
- Global Reach: Serves customers in 80+ countries through a network of distributors
- Comprehensive Solutions: Offers both fire trucks and specialized firefighting equipment
- Quality Manufacturing: Precision engineering and strict quality control processes
- Innovation in Pumps: Leading developments in pump efficiency and performance
- Hybrid and Electric Solutions: Early adoption of sustainable powertrain and pump technologies
- International Standards Compliance: Meets NFPA, ISO, and other global safety standards
- Support Services: Training, maintenance, and spare parts support worldwide
- Proven Reliability: Over 100 years of experience and trusted performance in critical operations
- Flexible Configurations: Fire trucks available on multiple chassis options for different needs
7. Toyota Auto Body Co., Ltd. (Fire Truck Division)
Based in Japan, Toyota Auto Body Co., Ltd. is a subsidiary of the Toyota Motor Corporation and a leading manufacturer of specialized vehicles, including fire trucks. The company has a long history of producing high-quality fire trucks for the Japanese market and has expanded its presence to international markets, particularly in Asia and Oceania. Toyota Auto Body’s fire trucks are renowned for their reliability, fuel efficiency, and advanced technology, leveraging Toyota’s expertise in automotive engineering and manufacturing.
Toyota Auto Body’s fire truck product line includes a variety of models, from compact urban fire engines to large aerial platforms and special rescue vehicles. The company uses Toyota’s chassis, known for their durability and fuel efficiency, combined with custom-built fire truck bodies and equipment. This integration of proven automotive technology with specialized firefighting equipment results in fire trucks that are reliable, easy to maintain, and fuel-efficient. Toyota Auto Body invests in developing advanced technologies for fire trucks, including hybrid powertrains, intelligent navigation systems, and safety features.
The company’s fire trucks are designed to meet Japanese industrial standards and international safety requirements, making them suitable for global markets. Toyota Auto Body’s manufacturing facilities in Japan employ advanced production techniques, ensuring high quality and consistency. The company also provides comprehensive after-sales support, including maintenance services and spare parts supply. In recent years, Toyota Auto Body has focused on developing electric fire trucks, aligning with global trends towards sustainable transportation and reducing emissions in urban areas.
Key Features and Advantages of Toyota Auto Body Co., Ltd. (Fire Truck Division)
- Toyota Engineering Leverage: Uses proven Toyota chassis and automotive technology for reliability
- Fuel Efficiency: Advanced engine and hybrid technologies reduce operating costs and emissions
- Compact and Agile Models: Well-suited for narrow urban streets and dense city environments
- Japanese Quality Standards: Strict manufacturing processes ensure high build quality and durability
- Electric Fire Truck Development: Leading in electric fire vehicle technology for urban areas
- Intelligent Features: Advanced navigation and operational systems for enhanced efficiency
- Global Market Access: Complies with international safety standards for export to Asia, Oceania, and beyond
- Reliable Support Network: Toyota’s global service infrastructure ensures spare parts and maintenance
- Hybrid Powertrains: Offers hybrid fire trucks that balance performance and fuel economy
- Innovation Focus: Develops technologies specific to urban firefighting challenges
8. Mercedes-Benz Special Trucks (Fire Truck Division)
Mercedes-Benz, a division of Daimler AG, is a globally recognized automotive manufacturer with a dedicated special trucks division producing fire trucks and emergency vehicles. Based in Germany, Mercedes-Benz Special Trucks has a long-standing reputation for manufacturing high-quality, reliable fire trucks that meet the demanding requirements of fire departments worldwide. The company combines Mercedes-Benz’s automotive expertise with specialized firefighting equipment to produce vehicles that excel in performance, safety, and comfort.
Mercedes-Benz’s fire truck product range includes various models, including the popular Atego, Actros, and Econic chassis, which are customized for firefighting applications. The Econic model is particularly well-regarded for fire trucks due to its low entry, panoramic windshield, and excellent visibility, making it ideal for urban firefighting operations. Mercedes-Benz works closely with fire truck body manufacturers to integrate specialized equipment such as pumps, water tanks, ladders, and rescue systems into their chassis, ensuring optimal performance and reliability.
The company invests in developing advanced technologies for its fire trucks, including intelligent safety systems, efficient engines, and connectivity features. Mercedes-Benz’s fire trucks are designed to meet strict European safety standards and are compliant with international regulations. The company’s global sales and service network ensures that customers receive timely support, spare parts, and maintenance services wherever they are located. Mercedes-Benz is also committed to sustainability, offering fire trucks with efficient diesel engines and developing electric special vehicles for emergency applications.
Key Features and Advantages of Mercedes-Benz Special Trucks (Fire Truck Division)
- Premium Automotive Engineering: Mercedes-Benz chassis known for reliability and performance
- Excellent Visibility: Models like Econic offer panoramic views and low entry for urban operations
- Advanced Safety Systems: Integrates modern driver assistance and safety technologies
- Global Service Network: Extensive worldwide sales and support infrastructure
- Fuel-Efficient Engines: Reduced operating costs and emissions through advanced engine technology
- Customization Options: Works with body manufacturers to tailor vehicles to specific fire department needs
- European Standards Compliance: Meets strict EU safety and performance requirements
- Comfortable Operation: Vehicle designs that reduce driver fatigue during long response times
- Electric Vehicle Development: Investing in electric special trucks for future emergency applications
- Proven Global Brand: Trusted name in automotive manufacturing with long-standing reliability
9. Iveco Magirus (Iveco Group)
Iveco Magirus, a joint venture between Iveco Group and Magirus GmbH, combines Iveco’s global truck manufacturing expertise with Magirus’ firefighting technology, creating a leading European supplier of fire trucks. Based in Ulm, Germany, Iveco Magirus leverages the strengths of both companies to produce high-quality fire trucks for markets across Europe and international clients. The company’s product range covers all types of fire trucks, from compact urban engines to large aerial platforms and specialized industrial vehicles.
Iveco Magirus uses Iveco’s robust truck chassis, designed for durability and performance, combined with Magirus’ specialized fire truck body technology and equipment. This synergy results in fire trucks that offer excellent maneuverability, reliability, and operational capability. The company’s product line includes pumpers, foam trucks, aerial ladders, platform trucks, and rescue vehicles, all designed to meet the specific needs of modern firefighting. Iveco Magirus invests in research and development, focusing on innovations that enhance firefighter safety, vehicle performance, and environmental sustainability.
The company’s fire trucks comply with strict European standards and are manufactured in state-of-the-art facilities in Germany. Iveco Magirus’ global distribution network ensures that customers worldwide have access to sales, support, and spare parts. The company has also been at the forefront of developing sustainable fire truck solutions, including natural gas-powered models and electric fire vehicles. Iveco Magirus’ combination of Iveco’s global reach and Magirus’ firefighting expertise makes it a strong competitor in the global fire truck market.
Key Features and Advantages of Iveco Magirus
- Synergistic Partnership: Combines Iveco’s global truck technology with Magirus’ firefighting expertise
- Wide Product Range: Covers all fire truck types to suit different operational needs
- European Manufacturing: State-of-the-art facilities ensuring quality and compliance
- Sustainable Solutions: Offers natural gas and electric fire trucks for lower emissions
- Global Distribution: Iveco’s worldwide network ensures international sales and support
- Maneuverability: Iveco chassis designs provide excellent handling for urban environments
- Safety Focus: Integrates Magirus’ firefighter safety systems with Iveco’s vehicle safety technology
- Customization: Flexible configurations to meet specific regional and department requirements
- Proven Reliability: Backed by two established brands with long histories in their sectors
- Innovation Investment: Focus on new technologies for improved performance and sustainability
10. Morita Holdings Corporation
Based in Tokyo, Japan, Morita Holdings Corporation is one of Asia’s leading manufacturers of fire trucks and firefighting equipment, with a history dating back to 1923. The company has built a strong reputation for high-quality, reliable fire trucks that serve fire departments across Japan, Asia, and other global markets. Morita is known for its innovative technology, particularly in fire pumps and water delivery systems, which are critical for effective firefighting operations.
Morita’s product portfolio includes a comprehensive range of fire trucks, including pumpers, foam trucks, aerial platforms, rescue vehicles, and specialized fire trucks for chemical, airport, and maritime applications. The company manufactures its fire trucks using chassis from leading Japanese and international brands, combined with custom-built bodies and specialized equipment. Morita’s fire pumps are renowned for their efficiency and reliability, with advanced designs that ensure consistent water flow even in demanding conditions. The company invests heavily in research and development, focusing on technologies that improve firefighter safety and operational effectiveness.
Morita’s manufacturing facilities in Japan adhere to strict quality control standards, ensuring that every fire truck meets the highest performance requirements. The company’s global network of distributors and service centers provides support to customers in over 50 countries. Morita has also developed electric fire trucks and hybrid systems, aligning with global trends towards sustainable transportation. The company’s strong presence in the Asian market and its commitment to innovation make it a key player in the global fire truck industry.
Key Features and Advantages of Morita Holdings Corporation
- Asian Market Leadership: Strong presence in Japan and across Asia’s growing fire service sector
- Fire Pump Expertise: Industry-leading pump technology for efficient water delivery
- Comprehensive Product Line: Covers all fire truck types including specialized industrial and airport models
- Japanese Quality Standards: Strict manufacturing and quality control processes
- Global Reach: Serves customers in 50+ countries through distributor network
- Electric and Hybrid Solutions: Early adoption of sustainable powertrain technologies
- Specialized Applications: Expertise in fire trucks for chemical, maritime, and airport environments
- Safety Innovation: Technologies designed to enhance firefighter safety during operations
- Proven Reliability: 100+ years of experience in firefighting equipment manufacturing
- Customer-Centric Approach: Works closely with fire departments to meet specific operational needs
Conclusion
The global fire truck industry in 2026 is characterized by a diverse range of suppliers that combine centuries of experience with cutting-edge technology to meet the evolving needs of emergency response organizations worldwide. The top 10 suppliers highlighted in this article represent a mix of global leaders and regional experts, each bringing unique strengths to the market. Hubei Ruitu Technology leads the way in combining competitive pricing with customization and innovation, making advanced firefighting equipment accessible to a wide range of customers. European suppliers like Rosenbauer, Magirus, Iveco Magirus, and Mercedes-Benz Special Trucks offer exceptional engineering quality, aerial technology leadership, and a strong focus on safety and sustainability. North American manufacturers such as E-one, Seagrave, and Darley America bring deep expertise in regional firefighting needs, heavy-duty applications, and compliance with strict safety standards. Japanese suppliers Toyota Auto Body and Morita contribute reliable, fuel-efficient vehicles and specialized technologies tailored to Asian and global markets.
What unites all these top suppliers is their commitment to innovation, quality, and customer service. As we move towards 2026, the industry is increasingly focused on developing electric and hybrid fire trucks, integrating smart technologies for better situational awareness, and improving firefighter safety through advanced designs and systems. The best fire truck suppliers understand that their products are critical for saving lives and protecting property, and they invest heavily in ensuring that their vehicles meet the highest performance standards. Whether a fire department needs a compact urban engine for narrow city streets, a large aerial platform for skyscraper firefighting, or a specialized vehicle for industrial or wildfire response, the top 10 suppliers in the world in 2026 have the expertise and capabilities to deliver solutions that meet their needs. The competitive landscape encourages continuous improvement, driving all suppliers to push the boundaries of technology and design, ultimately benefiting emergency response organizations and communities around the globe.